3.1 The Evolution of Industry 4.0 in Manufacturing Systems
Looking back, the story of manufacturing systems reads less like a single leap and more like a slow accumulation of small breaks with the past (Table 1). Craft-based production gave way, eventually, to mass production, standardized products, rigid workflows, and the economies of scale that came with assembly-line thinking (Hughes et al., 2022; Jamwal et al., 2021). Industry 3.0 then brought computerization: programmable logic controllers, SCADA systems, and early ERP platforms improved precision and departmental efficiency, but integration mostly stopped at the boundary of each department (Mathur et al., 2022). What none of these earlier phases achieved, and this is really the crux of it, was real-time, end-to-end coordination across the whole supply chain.
Industry 4.0 changes that equation. Cyber-physical systems, IoT, AI, and real-time data sharing together allow decision-making to become decentralized rather than centrally bottlenecked, and production systems to adapt on the fly rather than waiting for the next planning cycle (Andronie, Lăzăroiu, Ștefănescu, et al., 2021). The result, at least according to the sources reviewed here, is a supply chain that is more visible, more agile, and, perhaps most importantly for firms operating in volatile markets, more resilient than anything the earlier phases could offer.
3.2 Key Enabling Technologies
No single technology does all of this work alone (Table 2). IoT provides the connective tissue, linking physical assets to digital systems and enabling real-time visibility into where materials and products actually are (AlMetwally et al., 2020). Cyber-physical systems extend this further, integrating physical production equipment with digital control loops to support smart factories (Lee et al., 2020). Artificial intelligence and machine learning are where much of the analytical heavy lifting happens, demand forecasting, predictive maintenance, and process optimization all depend on these techniques translating raw sensor data into usable decisions (Andronie, Lăzăroiu, Iatagan, et al., 2021).
Big data analytics, meanwhile, is what makes sense of the sheer volume of information these systems generate, supporting the kind of data-driven decision-making that would otherwise be impossible at scale (Seyedan & Mafakheri, 2020). Cloud computing supplies the storage and computational backbone that lets partners across a supply chain share data without each maintaining separate, incompatible infrastructure (Li, 2022), and digital twins, virtual replicas of physical systems, allow companies to simulate different scenarios and catch risks before they materialize in the real world (Ivanov & Dolgui, 2021). Blockchain and robotics round out the picture: less central to the core narrative here, perhaps, but increasingly relevant for transaction transparency and physical task automation, respectively (Hellani et al., 2021; Fatima et al., 2022).
3.3 Supply Chain Process Mapping and Structure Mapping
These technologies onto an actual supply chain, from supplier through procurement, production, inventory, and distribution to the end customer, makes the transformation somewhat easier to see in concrete terms (Figure 1). What stands out is that the change is not confined to the physical flow of goods; it runs in parallel through an information flow (demand signals, production status, shipment tracking) and, layered above both, a decision flow that increasingly draws on data rather than static plans. Enabling technologies such as IoT, ERP systems, cloud computing, and AI reinforce this three-layer structure, and it is really the interaction between these layers, not any one layer alone, that produces the responsiveness Industry 4.0 is known for.
3.4 Demand Planning and Forecasting
Demand planning is perhaps where the shift from experience to evidence shows up most clearly (Figure 2).
Table 1. Evolution of Manufacturing Systems from Mechanization to Industry 4.0 in Smart Supply Chain Transformation Context.
|
Phase
|
Manufacturing Paradigm
|
Production Characteristics
|
Information Flow
|
Key Enabling Technologies
|
Supply Chain Characteristics
|
References
|
|
Pre-Industry 3.0 (Craft + Mechanization Era)
|
Craft-based and early mechanized production
|
Low standardization, labor-intensive, low scalability, high variability
|
Minimal digital information flow; paper-based coordination
|
Mechanical machines, steam power, basic electrification
|
Localized supply networks, long production cycles, low coordination between actors
|
(Mattiello & Rezaie, 2020)
|
|
Industry 2.0 (Mass Production Era)
|
Assembly line and standardized production
|
High volume production, standardized products, rigid workflows, economies of scale
|
Limited IT systems; functional silos in organizations
|
Electrical power, conveyor systems, Fordist assembly lines
|
Push-based supply chains, inventory accumulation, low flexibility
|
(Hughes et al., 2022; Jamwal et al., 2021)
|
|
Industry 3.0 (Automation & Computerization Era)
|
Automated and digitally controlled manufacturing
|
Machine-based automation, programmable systems, improved precision, partial integration
|
Digital but siloed systems (department-level integration only)
|
PLCs, SCADA, CAD/CAM, ERP systems, industrial robotics
|
Improved efficiency, better planning, but weak end-to-end visibility
|
(Mathur et al., 2022)
|
|
Industry 4.0 (Cyber-Physical Smart Manufacturing)
|
Smart, connected, autonomous manufacturing systems
|
Real-time responsiveness, mass customization, decentralized decision-making, self-optimizing systems
|
Seamless real-time data exchange across entire supply chain
|
IoT, Cyber-Physical Systems (CPS), AI/ML, Big Data, Cloud Computing.
|
Fully integrated, agile, demand-driven, transparent, resilient supply chains
|
(Andronie, Lăzăroiu, Ștefănescu, et al., 2021)
|
Table 2. Key Enabling Technologies of Industry 4.0 and Their Roles in Manufacturing Supply Chains.
|
Technology
|
Core Function in Industry 4.0
|
Application in Manufacturing Supply Chains
|
Key Benefit
|
References
|
|
Internet of Things (IoT)
|
Connects physical devices and enables real-time data collection
|
Machine monitoring, asset tracking, inventory visibility
|
Real-time visibility and tracking
|
(AlMetwally et al., 2020)
|
|
Cyber-Physical Systems (CPS)
|
Integration of physical systems with digital control
|
Smart factories, automated production control
|
Improved automation and coordination
|
(Lee et al., 2020)
|
|
Artificial Intelligence (AI) & Machine Learning
|
Data analysis and intelligent decision-making
|
Demand forecasting, predictive maintenance, optimization
|
Better decision accuracy and efficiency
|
(Andronie, Lăzăroiu, Iatagan, et al., 2021)
|
|
Big Data Analytics
|
Processing large and complex datasets
|
Supply chain optimization, performance analysis
|
Data-driven decision-making
|
(Seyedan & Mafakheri, 2020)
|
|
Cloud Computing
|
Scalable data storage and computing power
|
Cross-enterprise data sharing and collaboration
|
Improved connectivity and scalability
|
(Li, 2022)
|
|
Digital Twins
|
Virtual representation of physical systems
|
Simulation of production and supply chain processes
|
Scenario analysis and risk reduction
|
(Ivanov & Dolgui, 2021)
|
|
Blockchain Technology
|
Secure and transparent data exchange
|
Traceability, supplier verification, smart contracts
|
Enhanced transparency and trust
|
(Hellani et al., 2021)
|
|
Robotics & Automation
|
Physical task execution and process automation
|
Automated production lines, warehouse operations
|
Higher productivity and reduced human error
|
(Fatima et al., 2022)
|

Figure 1. End-to-end supply chain process mapping showing physical, information, and decision flows from supplier to customer, highlighting procurement, manufacturing, inventory, and distribution activities integrated with IoT, ERP, AI, and cloud-based enabling technologies for Industry 4.0 transformation.
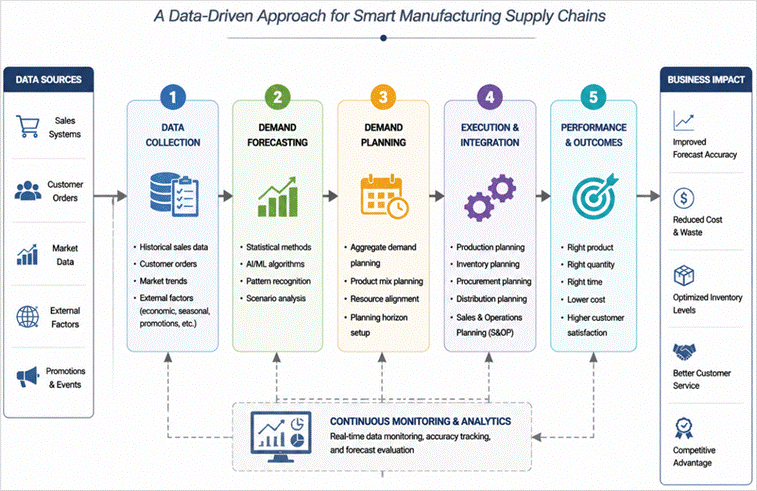
Figure 2. Data-driven demand planning and forecasting framework in manufacturing supply chains showing data collection, AI/ML-based forecasting, planning integration, execution processes, and continuous feedback enabled by Industry 4.0 technologies.
Table 3. Logistics and Distribution Management in Manufacturing Supply Chains.
|
Process
|
Objective
|
Key Activities
|
Inputs
|
Technology
|
KPI
|
Industry 4.0 Impact
|
References
|
|
Transportation Management
|
Efficient movement of goods
|
Route planning, carrier selection, shipment scheduling
|
Order data, shipment info
|
GPS, AI, IoT
|
Delivery time, transport cost
|
Real-time tracking, optimized routing
|
(Wan et al., 2018)
|
|
Order Fulfillment
|
Accurate and timely order delivery
|
Picking, packing, dispatching orders
|
Customer orders, inventory data
|
ERP, RFID, automation systems
|
Order accuracy, delivery speed
|
Integrated order processing system
|
(de Vass et al., 2021)
|
|
Warehouse Management
|
Efficient storage and handling
|
Stock control, picking, storage optimization
|
Inventory records
|
RFID, IoT sensors, robotics
|
Inventory turnover, space utilization
|
Smart warehouse operations
|
(Leng et al., 2021)
|
|
Distribution Network Management
|
Optimize product flow across network
|
Hub selection, distribution planning
|
Demand and logistics data
|
Big data analytics, digital twins
|
Lead time, distribution cost
|
AI-based network optimization
|
(Brusset et al., 2022)
|
|
Last-Mile Delivery
|
Final customer delivery efficiency
|
Delivery scheduling, tracking, communication
|
Shipment status, GPS data
|
GPS, drones, mobile apps
|
Customer satisfaction, delivery time
|
Real-time delivery visibility
|
(Zennaro et al., 2022)
|
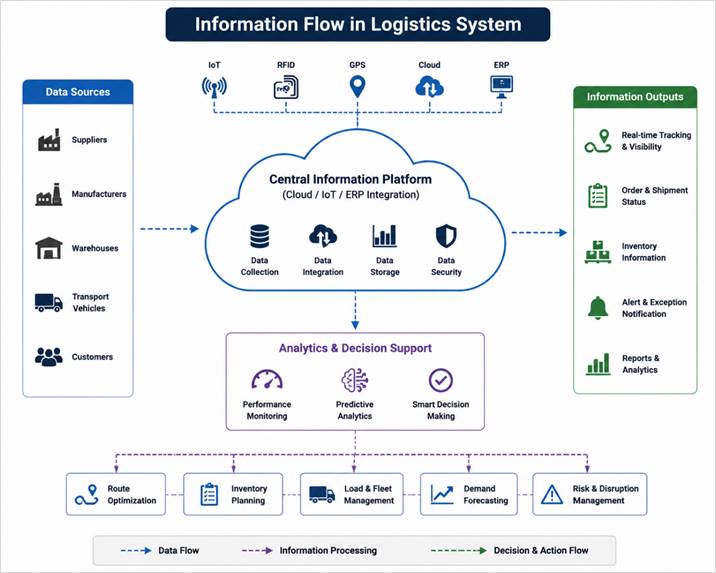
Figure 3. Information flow in logistics systems showing data collection from supply chain actors, integration through IoT/ERP/cloud platforms, and transformation into real-time analytics and decision support for improved logistics performance and Industry 4.0-enabled supply chain management.
Traditional forecasting relied heavily on historical sales patterns and, frankly, a fair amount of managerial judgment. The reviewed literature suggests a fairly consistent move away from that approach: sales data, market trends, and external signals are now fed through statistical models and AI or machine-learning algorithms capable of pattern recognition well beyond what manual analysis could achieve. Continuous monitoring closes the loop, letting firms compare forecasts against actual outcomes and adjust in near real time. Whether this consistently translates into lower costs and better customer service across firms of different sizes is less clear from the literature than the general direction of the trend, but the direction itself does seem well supported (Goli et al., 2022).
3.5 Logistics and Distribution Management
Logistics is where some of the more tangible, measurable gains appear (Table 3). Transportation management benefits from GPS and AI-driven route optimization; order fulfillment improves with RFID-enabled tracking through ERP systems; warehouse operations gain from IoT sensors and robotics that streamline stock control; and last-mile delivery, often the least efficient link in the chain, sees improvements from real-time tracking tools, including, in some cases, drones (Wan et al., 2018; Zennaro et al., 2022). Static planning, once the default in this domain, is being displaced by dynamic, data-informed routing that responds to demand fluctuations as they occur rather than after the fact.
3.6 Information Flow in Logistics Systems
Underlying all of the process-level gains discussed above is a less visible but arguably more foundational shift: how information itself moves through the system (Figure 3). Data from suppliers, manufacturers, warehouses, transport vehicles, and customers now converges on centralized platforms via IoT, RFID, GPS, cloud services, and ERP systems. This centralization is not merely a matter of convenience, it is what allows analytics and decision-support tools to convert raw, scattered inputs into forecasts, optimized routes, and risk assessments in something closer to real time. The practical effect, across the sources reviewed, is fewer delays and considerably better visibility into where things stand at any given moment.
3.7 Synthesis:
What This Means for Manufacturing Supply Chains Taken together, the evidence reviewed here points toward a fairly consistent conclusion: Industry 4.0 is not simply automating existing supply chain processes but restructuring how those processes relate to one another. The traditional, largely linear supply chain is giving way to something closer to an interwoven digital network, in which IoT, AI, big data, cyber-physical systems, cloud computing, and digital twins jointly enable real-time monitoring, predictive analysis, and increasingly autonomous decision-making (Lee et al., 2020; Radanliev et al., 2022; Stergiou & Psannis, 2022).
Improved visibility and coordination stand out as perhaps the most consistently reported benefit. Traditional systems suffer when communication lags, inventory piles up as a hedge against uncertainty, demand planning drifts out of sync with reality, and responses to disruption arrive late. Industry 4.0 technologies chip away at these problems by keeping data flowing continuously between nodes, and IoT sensors, RFID tagging, and cloud platforms combine to extend visibility from one end of the chain to the other, reducing uncertainty in the process (Coito et al., 2021; Ivanov & Dolgui, 2021). The net effect, several sources suggest, is a gradual shift from reactive operations toward proactive, and eventually predictive, ones.
This process-oriented lens also reveals that the impact is not uniform across functions. Procurement benefits from AI-supported supplier selection and risk assessment; production gains flexibility through cyber-physical systems and robotics; inventory management improves through predictive analytics that reduce holding costs; and logistics benefits from AI-based routing paired with real-time data (Cedillo-Campos et al., 2020; Jahani et al., 2021). None of these gains, though, happen in isolation, the coordination between functions, enabled by shared digital infrastructure, appears to matter as much as any single technology's contribution to any single process.
A further theme worth dwelling on is the growing centrality of data itself as a strategic asset. Big data analytics allows firms to convert large, messy datasets, much of it unstructured, into forecasts and production schedules with a level of precision that would have been unreasonable to expect a decade ago. Machine learning algorithms, in particular, seem able to surface patterns in this data that human analysts would likely miss, and digital twins add a further layer by letting firms simulate scenarios and anticipate risks before committing resources (Brintrup et al., 2020; Cedillo-Campos et al., 2020; Ivanov & Dolgui, 2021).
None of this is free of friction, however, and it would be a disservice to the literature to gloss over the obstacles. Implementation costs remain a genuine barrier, disproportionately so for small and medium-sized enterprises that lack the capital of larger competitors. Interconnectedness, while it enables visibility, also expands the attack surface for cyber threats, and data privacy concerns compound the challenge (Masip-Bruin et al., 2021; Melnyk et al., 2022; Radanliev et al., 2020). Interoperability between legacy systems and newer digital tools remains unresolved in many organizations, and a persistent shortage of workers skilled enough to operate these systems continues to slow adoption, a constraint that, if anything, seems underappreciated relative to the attention given to the technologies themselves.
Finally, the reviewed literature converges on a point that is easy to overlook amid the technical detail: successful Industry 4.0 adoption is not purely a technology problem. Organizations need a decision-making culture that actually trusts and uses the data these systems generate, along with sustained investment in workforce training. Getting the technology right without getting the people and processes right alongside it appears, from this review, to be a recipe for underperformance rather than transformation.